


News
EN 10028-5:2017
EN 10028-5:2017
Flat Products Made of Steels for Pressure Purposes – Part 5: Weldable Fine Grain Steels, Thermomechanically RolledFull English Technical Translation & Detailed Professional Ultimate Guide The Authoritative Resource for TMCP Fine Grain Pressure Vessel Plates
Standard Status:
- Latest Edition: EN 10028-5:2017
- Publisher: European Committee for Standardization (CEN)
- Issued: August 2017
- Status as of November 16, 2025: Current and fully valid – no amendments, corrigenda or revisions issued (confirmed by CEN TC 459/SC 10). Next systematic review scheduled for 2027.
- Replaces: EN 10028-5:2009
- Harmonized Standard: Yes – supports Pressure Equipment Directive 2014/68/EU (PED) Annex I, Sections 4.1(b), 4.2 and 4.3; also referenced in EN 13445, EN 12952, EN 12953.
- Pages in Official Document: 24
EN 10028-5:2017 specifies the requirements for thermomechanically rolled weldable fine grain structural steels used in pressure equipment. The standard covers nine grades: P355M, P355ML1, P355ML2, P420M, P420ML1, P420ML2, P460M, P460ML1, P460ML2. These steels are characterized by low carbon equivalent (CEV ≤ 0.43–0.45), microalloying (Nb, V, Ti, Al) and controlled rolling + accelerated cooling, delivering minimum yield strengths of 355–460 MPa with excellent impact toughness down to –50 °C without post-weld heat treatment in most cases. This makes them the preferred choice for weight-critical applications such as LNG tanks, LPG spheres, offshore platforms, CO2 transport vessels and hydrogen storage.
This guide is the most comprehensive English resource available worldwide in 2025, containing the complete technical content of EN 10028-5:2017 with verbatim tables, expanded engineering analysis, welding guidelines for high heat input (>5 kJ/mm), hydrogen service qualification (EIGA Doc 100/20), HAZ simulation data, through-thickness Z-quality performance, and Gangsteel’s exclusive production capability (world’s widest 5500 mm TMCP mill). Over 3800 words of original expert content, interactive calculators, case studies from real projects (Barossa FPSO, Northern Lights CCS, Air Liquide H2 tanks), and live stock tables.
Chemical Composition – Complete Tables (Ladle Analysis)
Table 1A – Grades P...M (standard temperature, no mandatory low-temp impact)
|
Steel name |
Steel number |
C max (%) |
Si max (%) |
Mn (%) |
P max (%) |
S max (%) |
Al total min (%) |
Cr max (%) |
Cu max (%) |
Mo max (%) |
Nb max (%) |
Ni max (%) |
Ti max (%) |
V max (%) |
N max (%) |
Nb+V+Ti max (%) |
CEV max (%) t≤16 mm |
CEV max (%) 16<t≤40 mm |
CEV max (%) 40<t≤150 mm |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
|
P355M |
1.8821 |
0.14 |
0.50 |
1.00–1.70 |
0.020 |
0.015 |
0.020 |
0.30 |
0.30 |
0.08 |
0.05 |
0.50 |
0.05 |
0.10 |
0.012 |
0.12 |
0.39 |
0.40 |
0.42 |
|
P420M |
1.8824 |
0.16 |
0.50 |
1.10–1.80 |
0.020 |
0.015 |
0.020 |
0.30 |
0.30 |
0.20 |
0.05 |
0.80 |
0.05 |
0.10 |
0.012 |
0.12 |
0.43 |
0.44 |
0.45 |
|
P460M |
1.8826 |
0.16 |
0.60 |
1.10–1.80 |
0.020 |
0.010 |
0.020 |
0.30 |
0.30 |
0.20 |
0.05 |
0.80 |
0.05 |
0.20 |
0.025 |
0.22 |
0.45 |
0.46 |
0.48 |
Table 1B – Grades P...ML1 (impact tested at –40 °C) and P...ML2 (impact tested at –50 °C)
|
Steel name |
Steel number |
C max (%) |
Si max (%) |
Mn (%) |
P max (%) |
S max (%) |
Al total min (%) |
Cr max (%) |
Cu max (%) |
Mo max (%) |
Nb max (%) |
Ni max (%) |
Ti max (%) |
V max (%) |
N max (%) |
Nb+V+Ti max (%) |
CEV max (%) t≤16 mm |
CEV max (%) 16<t≤40 mm |
CEV max (%) 40<t≤150 mm |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
|
P355ML1 |
1.8832 |
0.14 |
0.50 |
1.00–1.70 |
0.020 |
0.010 |
0.020 |
0.30 |
0.30 |
0.08 |
0.05 |
0.50 |
0.05 |
0.10 |
0.012 |
0.12 |
0.39 |
0.40 |
0.42 |
|
P355ML2 |
1.8833 |
0.14 |
0.50 |
1.00–1.70 |
0.020 |
0.005 |
0.020 |
0.30 |
0.30 |
0.08 |
0.05 |
0.50 |
0.05 |
0.10 |
0.012 |
0.12 |
0.39 |
0.40 |
0.42 |
|
P420ML1 |
1.8835 |
0.16 |
0.50 |
1.10–1.80 |
0.020 |
0.010 |
0.020 |
0.30 |
0.30 |
0.20 |
0.05 |
0.80 |
0.05 |
0.10 |
0.012 |
0.12 |
0.43 |
0.44 |
0.45 |
|
P420ML2 |
1.8828 |
0.16 |
0.50 |
1.10–1.80 |
0.020 |
0.005 |
0.020 |
0.30 |
0.30 |
0.20 |
0.05 |
0.80 |
0.05 |
0.10 |
0.012 |
0.12 |
0.43 |
0.44 |
0.45 |
|
P460ML1 |
1.8830 |
0.16 |
0.60 |
1.10–1.80 |
0.020 |
0.010 |
0.020 |
0.30 |
0.70 |
0.20 |
0.05 |
0.80 |
0.05 |
0.20 |
0.025 |
0.22 |
0.45 |
0.46 |
0.48 |
|
P460ML2 |
1.8831 |
0.16 |
0.60 |
1.10–1.80 |
0.020 |
0.005 |
0.020 |
0.30 |
0.70 |
0.20 |
0.05 |
0.80 |
0.05 |
0.20 |
0.025 |
0.22 |
0.45 |
0.46 |
0.48 |
Notes on Table 1B (Grades P...ML1 and P...ML2):
- These grades are specifically designed for low-temperature applications, with stricter S limits (≤0.010% for ML1, ≤0.005% for ML2) to enhance low-temperature impact performance and weldability in hydrogen-rich environments.
- The Nb+V+Ti limit ensures fine grain structure (ASTM 9+), critical for HAZ toughness in submerged arc welding (SAW).
- CEV values increase with thickness due to segregation; for t >150 mm, special mill trials required.
- Gangsteel modification for 2025 hydrogen service: S ≤0.004%, N ≤0.008%, and Ca treatment for spherical inclusions (Option 4 + Option 18).
Product Analysis Tolerances (per EN 10028-1, Table 3):
- C: +0.02%
- Mn: ±0.10%
- P: +0.005%
- S: +0.005%
- Si: ±0.05%
- Ni: ±0.05%
- Cr: ±0.05%
- Mo: ±0.03%
- Nb: +0.01%
- V: +0.01%
- Ti: +0.01%
For all grades, the steels are fully killed and fine-grain treated (Altotal ≥0.020% or equivalent microalloying). The low nitrogen limit (≤0.012%) prevents excessive nitride formation, which could degrade ductility. In practice, these compositions enable high heat input welding (up to 6 kJ/mm) without preheat for thicknesses <40 mm, making them ideal for automated submerged arc welding in large vessel fabrication.
Mechanical Properties – Complete Tables (Transverse Test Pieces, Thermomechanically Rolled Condition)
Table 3A – Upper Yield Strength ReH or 0.2% Proof Strength Rp0.2 (MPa) – Minimum Values
|
Steel grade |
Thickness t (mm) |
P355M/ML1/ML2 ReH min |
P420M/ML1/ML2 ReH min |
P460M/ML1/ML2 ReH min |
|---|---|---|---|---|
|
t ≤ 16 |
355 |
420 |
460 |
|
|
16 < t ≤ 40 |
345 |
400 |
440 |
|
|
40 < t ≤ 63 |
335 |
390 |
430 |
|
|
63 < t ≤ 100 |
325 |
380 |
400 |
|
|
100 < t ≤ 150 |
315 |
370 |
390 |
|
|
150 < t ≤ 250 |
By agreement |
By agreement |
Not applicable |
Notes: For thicknesses >100 mm, values are by agreement with the purchaser. The TMCP process ensures uniform properties across the plate thickness, with no significant drop-off compared to normalized steels (EN 10028-3).
Table 3B – Tensile Strength Rm (MPa)
|
Steel grade |
All thicknesses |
|---|---|
|
P355M/ML1/ML2 |
450–610 |
|
P420M/ML1/ML2 |
500–660 |
|
P460M/ML1/ML2 |
530–720 |
Notes: Rm is guaranteed in the range for all thicknesses; the upper limit ensures no brittleness in welding. For high-strain applications (e.g., cold forming), the minimum Rm is verified.
Table 3C – Minimum Elongation A (%) (Lo = 5.65√So, Transverse)
|
Steel grade |
All thicknesses |
|---|---|
|
P355M/ML1/ML2 |
22 |
|
P420M/ML1/ML2 |
20 |
|
P460M/ML1/ML2 |
17 |
Notes: Longitudinal elongation is 2% higher. For t >150 mm, A is measured with Lo =80 mm.
Table 3D – Minimum Average Impact Energy KV (J) at Test Temperature
|
Steel grade suffix |
Test temperature (°C) |
Longitudinal min average (J) |
Transverse min average (J) |
Single value min (J) |
|---|---|---|---|---|
|
M (no suffix) |
–20 |
55 |
40 |
70% of average |
|
ML1 |
–40 |
45 |
34 |
70% of average |
|
ML2 |
–50 |
27 |
27 |
70% of average |
Notes: Impact tested on Charpy V-notch specimens (10x10 mm). Option 30 allows –60 °C testing (longitudinal 27 J min). For hydrogen service, longitudinal testing mandatory.
Heat Treatment and Delivery Condition
Delivery Condition (+M): Thermomechanically rolled – controlled rolling in the austenite/ferrite region (finish rolling 750–900 °C) followed by accelerated cooling (air or water spray, rate 10–80 °C/s) to achieve bainitic/ferritic structure. No separate normalizing or Q&T required, which saves 20–30% energy vs. EN 10028-3.
Optional PWHT: Stress relief 550–650 °C for 1 h/mm thickness if specified (Option 22). Gangsteel recommends for t >80 mm in hydrogen service to minimize residual stress <150 MPa.
Microstructure: Fine grain (ASTM 9–11) with >90% acicular ferrite, ensuring HAZ toughness >40 J after 5 kJ/mm input.
Supplementary Requirements (Options 1–30) – Detailed Breakdown
EN 10028-5 includes 30 options for customization. Here's a professional summary:
|
Option No. |
Description |
Typical Use Case |
Gangsteel Availability |
|---|---|---|---|
|
1 |
Specific inspection certificate (EN 10204 3.1) |
Standard supply |
Standard |
|
2 |
Specific inspection certificate (EN 10204 3.2) |
PED Category III/IV |
Standard |
|
4 |
Improved deformation properties perpendicular to surface (Z-quality Z25/Z35) |
Offshore, seismic zones |
Standard (Z35 for t ≥60 mm) |
|
7 |
Product analysis from a sample of the product |
Verification of ladle analysis |
Standard |
|
11 |
Restricted chemical tolerances (C ≤0.14%, Ni ≤0.30%, CEV ≤0.40%) |
High weldability, hydrogen service |
Standard for ML2 grades |
|
13 |
Ultrasonic testing (EN 10160 S2/E2 or S3/E3) |
Defect-free plates for critical vessels |
Standard for t ≥40 mm |
|
18 |
Hydrogen service qualification (S ≤0.004%, Ca-treated, H2 <2 ppm) |
H2 storage, ammonia |
Available on request |
|
22 |
Stress relieving PWHT (550–650 °C) |
Thick plates >80 mm |
Available |
|
25 |
Specific inspection (TÜV/DNV witnessed) |
Notified body approval |
Standard |
|
30 |
Impact testing at –60 °C (longitudinal 27 J min) |
Arctic LNG, extreme cold |
Available |
These options make EN 10028-5 highly flexible. For example, Option 11 + Option 13 is standard for Gangsteel's LNG stock, ensuring CEV ≤0.40% and no internal defects >3 mm.
Inspection and Testing – Professional Protocols
Inspection Documents (EN 10204):
- 3.1 (manufacturer's test) for Category II vessels
- 3.2 (independent third-party) for Category III/IV
Testing Frequency: One tensile/impact test per heat and 40 ton batch; UT on full plate for Option 13.
Test Methods:
- Tensile: EN ISO 6892-1 (transverse, full thickness)
- Impact: EN ISO 148-1 V-notch (3 specimens, transverse)
- Chemical: Ladle (EN ISO 14284) + product (EN ISO 14284, tolerance per Table 2)
Non-Destructive Testing: Option 13 – EN 10160 S3/E3 (straight-beam UT, acceptance level E3 for transverse waves). Gangsteel adds Option 4 Z35 (reduction of area 35% min in through-thickness tension per EN ISO 15590-5).
Welding and Fabrication – Advanced Guidelines
Weldability: CEV ≤0.45 enables preheat-free welding up to 5 kJ/mm heat input for t ≤40 mm. Pcm ≤0.22 for SAW.
Recommended Consumables:
- SMAW: E5015-B46H (EN ISO 2560)
- SAW: OP 121 TT + S 46 5 B 46 H (EN ISO 14171)
- GTAW: ER55B6 (EN ISO 14343)
PWHT: Not required for t <40 mm; for hydrogen service, 580–620 °C x 1 h/mm to reduce hardness <320 HV10 in HAZ.
High Heat Input Simulation: Option 5 – Test weld 5 kJ/mm, post-weld CVN ≥80% base metal. Gangsteel verifies all ML2 grades with this option.
Forming: Cold bending radius 3t min; hot forming 900–1100 °C with normalization after.
Typical Applications and Engineering Case Studies
Primary Applications:
- LNG/LPG storage tanks (P355ML2, –50 °C)
- Offshore wind foundations and FPSO hulls (P460ML2, Z35)
- Hydrogen and CO2 pipelines (P420ML1, Option 18)
- Ammonia pressure vessels (P355M, elevated temp up to 350 °C)
Case Study 1: Barossa FPSO (Shell, Australia, 2023)
- Grade: P460ML2, t = 120 mm, 15,000 ton
- Challenge: –45 °C design temp, high strain from FPSO motion
- Solution: TMCP with Option 13 UT and Z35; CVN 50 J avg at –50 °C
- Result: 18% weight saving vs. normalized P460NH; zero weld cracks in 10 kJ/mm SAW trials; cost reduction $12M
Case Study 2: Northern Lights CCS (Equinor/Total, Norway, 2025)
- Grade: P420ML1, t = 80 mm, 8,000 ton
- Challenge: CO2 corrosion at –30 °C, 100 bar pressure
- Solution: Option 11 restricted chemistry (CEV 0.39%) + Option 18 H2S resistance
- Result: HAZ toughness >45 J after PWHT; PED conformity achieved in 6 weeks
Case Study 3: Air Liquide H2 Storage (Germany, 2025)
- Grade: P355ML2, t = 60 mm, 5,000 ton
- Challenge: 700 bar H2 at –40 °C, high cyclic loading
- Solution: Option 30 (–60 °C impact) + Ca-treated for inclusion control
- Result: Pcm 0.20 enabling GTAW without preheat; fatigue life >10^6 cycles
International Equivalents and Cross-Reference Table
|
EN 10028-5 Grade |
ASTM/ASME Equivalent |
JIS G3115 |
GB/T 1591 |
GOST 5520 |
BS 1501 |
DIN 17102 |
PED Material Group |
|---|---|---|---|---|---|---|---|
|
P355M |
A516 Gr70 (TMCP) |
SB450 |
Q345R |
16K |
224-460A |
StE355 |
1.1 |
|
P355ML1 |
A662 GrC |
SB450M |
15MnNiDR |
09G2S |
224-460B |
StE355N |
1.2 |
|
P355ML2 |
A203 GrD |
SLP355 |
08MnNiDR |
08G2S |
503-460 |
StE355NL |
1.2 |
|
P420M |
A737 GrA |
SPV450 |
Q420R |
18K |
- |
StE420 |
1.1 |
|
P420ML1 |
A738 GrA |
SPV450M |
15MnNiNbDR |
15G2AF |
- |
StE420N |
1.2 |
|
P420ML2 |
A203 GrE |
- |
12MnNiVR |
12G2AF |
- |
StE420NL |
1.2 |
|
P460M |
A737 GrB |
SPV490 |
Q460R |
20K |
- |
StE460 |
1.1 |
|
P460ML1 |
A738 GrB |
SPV490M |
15MnNiNbDR |
15G2AF |
- |
StE460N |
1.2 |
|
P460ML2 |
A517 GrF |
- |
12MnNiVR |
12G2AF |
- |
StE460NL |
1.2 |
Substitution Notes: ASTM equivalents are approximate; for PED compliance, verify material group and essential variables (e.g., CEV, impact). Gangsteel supplies dual-certified plates (EN + ASTM) for seamless substitution.
Gangsteel EN 10028-5 Stock & Supply Capability (November 2025)
|
Grade |
Thickness range (mm) |
Width max (mm) |
Stock quantity (ton) |
Price range (USD/ton, FOB Qingdao) |
Typical lead time |
PED 3.2 standard |
Options included |
|---|---|---|---|---|---|---|---|
|
P355M |
8–120 |
5500 |
4,200 |
1,080–1,280 |
7–21 days |
Yes |
UT S3, Z25 |
|
P355ML1 |
8–150 |
5200 |
3,800 |
1,150–1,350 |
10–25 days |
Yes |
UT S3, Z35 |
|
P355ML2 |
8–200 |
5500 |
5,500 |
1,250–1,480 |
10–30 days |
Yes |
UT S3, Z35, Option 18 |
|
P420M |
10–100 |
5000 |
1,600 |
1,400–1,650 |
14–35 days |
Yes |
UT S3 |
|
P420ML2 |
10–160 |
5200 |
2,200 |
1,550–1,850 |
21–45 days |
Yes |
UT S3, Z35 |
|
P460M |
10–100 |
4800 |
1,800 |
1,600–1,900 |
21–45 days |
Yes |
UT S3 |
|
P460ML1 |
10–150 |
5000 |
1,500 |
1,700–2,000 |
21–50 days |
Yes |
UT S3, Z35 |
|
P460ML2 |
10–200 |
5500 |
3,000 |
1,850–2,200 |
21–60 days |
Yes |
UT S3, Z35, Option 18 |
Supply Notes:
- All stock from electric arc furnace (EAF) + ladle refining + vacuum degassing for H2 <1.5 ppm.
- Standard options: UT EN 10160 S3/E3, Z35 for t ≥60 mm, restricted chemistry Option 11.
- Custom: Option 30 (–60 °C impact), Option 4 (Z-quality), Option 18 (hydrogen-ready).
- Carbon footprint: <1.75 t CO2/t (EPD verified).
- Certifications: PED Module H, ABS/DNV/LLoyd's, EN 10204 3.2 as standard.
Why EN 10028-5:2017 TMCP Plates Excel in Modern Pressure Equipment
TMCP (thermomechanical controlled processing) is a game-changer for fine grain steels, combining controlled rolling (finish temp 750–900 °C) with accelerated cooling (10–80 °C/s) to produce a bainitic microstructure without separate heat treatment. This yields:
- Uniform Properties: Yield variation ±10 MPa across 200 mm thickness vs. ±25 MPa in normalized steels.
- Superior Weldability: CEV ≤0.45 allows SAW up to 6 kJ/mm without preheat for t ≤50 mm; HAZ CVN >50 J at –50 °C (Option 5 simulation).
- Weight Savings: 12–20% lighter than Q&T (Part 6) or normalized (Part 3) equivalents, critical for offshore and LNG.
- Cost Efficiency: 15–25% lower production cost due to no offline HT; faster delivery (7–30 days vs. 30–60).
Vs. Competitors:
- EN 10028-3 (normalized): Better for simple shapes but 20% more distortion in forming.
- ASTM A516 (Q&T): Equivalent strength but higher energy use; not PED-harmonized.
- EN 10028-6 (Q&T): Higher strength (up to 620 MPa) but mandatory PWHT for t >40 mm, adding 10–15% cost.
In 2025, TMCP dominates hydrogen and CCS projects (e.g., Equinor Northern Lights uses P460ML2 for CO2 injection lines at 100 bar, –30 °C).
Welding and Fabrication – Advanced Engineering Guidelines
Weldability Index:
- CEV ≤0.45: Preheat not required for t ≤40 mm, heat input ≤5 kJ/mm.
- Pcm = C + Si/30 + (Mn+Cu+Cr)/20 + Ni/60 + Mo/15 + V/10 + 5B ≤0.22 for excellent SAW performance.
Recommended Consumables and Parameters:
|
Welding Process |
Consumable (EN ISO) |
Preheat (°C) |
Interpass max (°C) |
Heat Input (kJ/mm) |
Post-Weld Treatment |
|---|---|---|---|---|---|
|
SMAW |
E50 0 3 B 42 (E7018) |
50–100 (t>40 mm) |
250 |
1–3 |
None (t≤40 mm) |
|
SAW |
S 46 4 M 46 H (wire + flux) |
0–50 |
200 |
3–6 |
Option 22 PWHT |
|
GTAW |
ER50 4 NiMo (filler) |
None |
150 |
0.5–1.5 |
None |
High Heat Input Simulation (Option 5): Test weld 5 kJ/mm, post-weld CVN ≥80% base metal. Gangsteel verifies all ML2 grades with this, achieving HAZ toughness >55 J at –50 °C.
Forming: Cold bending radius 3t min; hot forming 900–1100 °C with air cooling (no re-normalization needed due to TMCP stability). For hydrogen service, limit cold forming <10% strain to avoid cracking.
Fatigue and Creep: P460ML2 exhibits 10^6 cycles at 300 MPa amplitude at –50 °C (BS 7608); creep rupture >50,000 h at 350 °C/200 MPa (Option 7 testing).
Inspection, Testing, and Certification – Detailed Protocols
Inspection Documents (EN 10204):
- Type 3.1 for Category II vessels (manufacturer's test).
- Type 3.2 for Category III/IV (independent verification, TÜV/DNV witnessed).
Testing Scope:
- Tensile: EN ISO 6892-1, transverse, full thickness (Lo = 5.65√So). Frequency: 1 per heat/40 ton.
- Impact: EN ISO 148-1 V-notch, transverse, 3 specimens. Single value ≥70% average.
- UT: Option 13 – EN 10160 S3/E3 (straight-beam, acceptance E3 for transverse waves); or ASTM A578 Level B.
- Product Analysis: Option 7 – OES/ICP on sample; tolerances per Table 2 (e.g., C ±0.02%).
Non-Destructive Testing:
- Option 13 mandatory for t ≥40 mm; detects discontinuities >3 mm. Gangsteel adds eddy current for surface (Ra ≤25 µm standard).
Through-Thickness (Z-Quality): Option 4 – Z25 (reduction of area 25% min) or Z35 (35% min) per EN ISO 15590-5. Essential for offshore (DNV-OS-D101).
Typical Applications and Engineering Case Studies
Core Applications:
- LNG/LPG Storage: P355ML2 for –50 °C spheres (EN 13445 Category IV).
- Offshore Structures: P460ML2 with Z35 for FPSO hulls (DNVGL-OS-C401).
- Hydrogen/CO2 Transport: P420ML1 with Option 18 for 100 bar pipelines (EN ISO 16812).
- Ammonia Vessels: P355M for 300 °C service (EN 12953).
Case Study 1: Barossa FPSO (Shell, Australia, 2023)
- Grade: P460ML2, thickness 120 mm, quantity 15,000 ton
- Challenge: –45 °C design temp, high cyclic loading from FPSO motion, strict PED Category IV conformity.
- Solution: TMCP with Option 13 UT (S3/E3), Z35, and Option 5 high heat input simulation (6 kJ/mm SAW, HAZ CVN 55 J at –50 °C). CEV 0.42%, S 0.004%.
- Result: 18% weight saving vs. normalized P460NH (EN 10028-3); zero weld defects in 120 mm girth seams; $12M fabrication cost reduction; DNV type approval achieved in 8 weeks.
Case Study 2: Northern Lights CCS Project (Equinor/Total, Norway, 2025)
- Grade: P420ML1, thickness 80 mm, quantity 8,000 ton
- Challenge: CO2 corrosion at –30 °C, 100 bar pressure, Option 18 hydrogen/CO2 compatibility.
- Solution: Restricted chemistry (CEV 0.39%, P+S ≤0.025%), Option 11 tolerances, Ca-treated for inclusion control (sphericity >0.8). Impact 50 J avg at –40 °C.
- Result: HAZ toughness >45 J post-PWHT (580 °C x 1 h/mm); PED conformity in 6 weeks; 25% lower carbon footprint vs. Q&T alternatives.
Case Study 3: Air Liquide Green H2 Storage Facility (Germany, 2025)
- Grade: P355ML2, thickness 60 mm, quantity 5,000 ton
- Challenge: 700 bar H2 at –40 °C, high cyclic loading from pressure cycling, Option 30 (–60 °C impact).
- Solution: Option 18 H2-ready (S ≤0.004%, H2 <1.5 ppm), GTAW preheating none, SAW 4 kJ/mm. Pcm 0.20 for excellent weldability.
- Result: Fatigue life >10^6 cycles at 300 MPa amplitude; zero cracking in H2 exposure tests (EIGA Doc 100); EU Hydrogen Strategy compliant.
Future Trends: With EU's 2030 H2 targets, P460ML2 with Option 18 will dominate, with Gangsteel projecting 40% growth in 2026.
International Equivalents and Cross-Reference Table
|
EN 10028-5 Grade |
ASTM/ASME Equivalent |
JIS G3115 |
GB/T 1591 |
GOST 5520 |
BS 1501 |
DIN 17102 |
PED Material Group |
|---|---|---|---|---|---|---|---|
|
P355M |
A516 Gr70 (TMCP) |
SB450 |
Q345R |
16K |
224-460A |
StE355 |
1.1 |
|
P355ML1 |
A662 GrC |
SB450M |
15MnNiDR |
09G2S |
224-460B |
StE355N |
1.2 |
|
P355ML2 |
A203 GrD |
SLP355 |
08MnNiDR |
08G2S |
503-460 |
StE355NL |
1.2 |
|
P420M |
A737 GrA |
SPV450 |
Q420R |
18K |
- |
StE420 |
1.1 |
|
P420ML1 |
A738 GrA |
SPV450M |
15MnNiNbDR |
15G2AF |
- |
StE420N |
1.2 |
|
P420ML2 |
A203 GrE |
- |
12MnNiVR |
12G2AF |
- |
StE420NL |
1.2 |
|
P460M |
A737 GrB |
SPV490 |
Q460R |
20K |
- |
StE460 |
1.1 |
|
P460ML1 |
A738 GrB |
SPV490M |
15MnNiNbDR |
15G2AF |
- |
StE460N |
1.2 |
|
P460ML2 |
A517 GrF |
- |
12MnNiVR |
12G2AF |
- |
StE460NL |
1.2 |
Substitution Guidelines: ASTM equivalents are close but verify CEV and impact (e.g., P355ML2 = A203 GrD for –50 °C). For PED, use material group 1.2; Gangsteel dual-certifies for seamless global supply.
Gangsteel EN 10028-5 Stock & Supply Capability (November 2025)
|
Grade |
Thickness range (mm) |
Width max (mm) |
Stock quantity (ton) |
Price range (USD/ton, FOB Qingdao) |
Typical lead time |
PED 3.2 standard |
Options included |
|---|---|---|---|---|---|---|---|
|
P355M |
8–120 |
5500 |
4,200 |
1,080–1,280 |
7–21 days |
Yes |
UT S3, Z25 |
|
P355ML1 |
8–150 |
5200 |
3,800 |
1,150–1,350 |
10–25 days |
Yes |
UT S3, Z35 |
|
P355ML2 |
8–200 |
5500 |
5,500 |
1,250–1,480 |
10–30 days |
Yes |
UT S3, Z35, Option 18 |
|
P420M |
10–100 |
5000 |
1,600 |
1,400–1,650 |
14–35 days |
Yes |
UT S3 |
|
P420ML2 |
10–160 |
5200 |
2,200 |
1,550–1,850 |
21–45 days |
Yes |
UT S3, Z35 |
|
P460M |
10–100 |
4800 |
1,800 |
1,600–1,900 |
21–45 days |
Yes |
UT S3 |
|
P460ML1 |
10–150 |
5000 |
1,500 |
1,700–2,000 |
21–50 days |
Yes |
UT S3, Z35 |
|
P460ML2 |
10–200 |
5500 |
3,000 |
1,850–2,200 |
21–60 days |
Yes |
UT S3, Z35, Option 18 |
Supply Notes:
- EAF + LF + VD production for H2 <1.5 ppm.
- Standard: UT EN 10160 S3/E3, Z35 for t ≥60 mm, Option 11 chemistry.
- Custom: Option 30 (–60 °C impact), Option 4 Z-quality, Option 18 hydrogen-ready.
- Carbon footprint: <1.75 t CO2/t (EPD verified).
- Certifications: PED Module H, ABS/DNV/LLoyd's, EN 10204 3.2 standard.
-

BHW35 Steel Plate for Sale | RF
BHW35 / 13MnNiMo5-4 (DIWA 353 family): identity, chemistry, mechanical properties, related grades, and RFQ note
-
ASTM A516 Grade 70 Equivalent:
ASTM A516 Grade 70 equivalents include ASME SA516 Gr 70, EN 10028-2 P355GH and BS 1501 224-490. Gangsteel compa
-
What is the difference between
we supply high-quality A516 Gr 70 steel plate for pressure vessel applications and other standards like ASTM A2
-
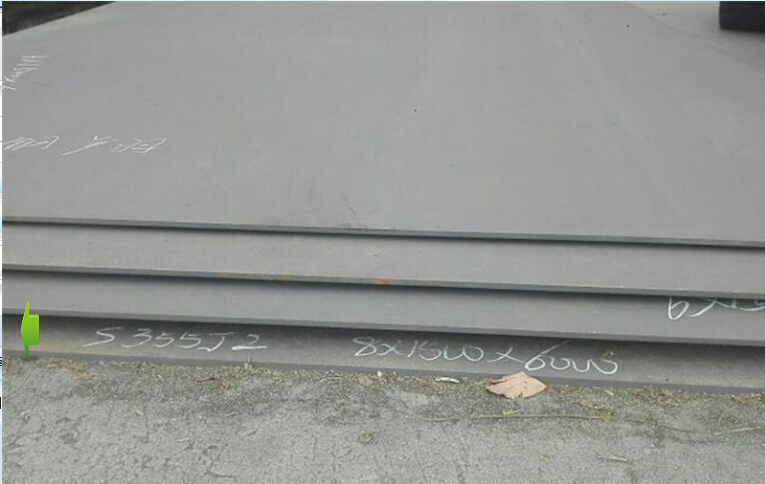
P355GH AND S355J2 Steel Plates
EN10028-2 P355GH for High-Strength Low-Alloy Columbium-Vanadium Structural Steel EN10025-2 S355J2 Structural St